Most logistics procurement managers don’t set out to reduce moving bag failures — until a quarter’s damage claims hit the desk and the math gets ugly. One regional moving firm watched its annual procurement tab climb past $12,600 while crews lost hours repacking loads that tore through standard woven PP bags mid-route. The bags weren’t supposed to fail. The spec sheets said they wouldn’t. The field told a different story, and the gap between lab numbers and real-world dynamic load performance was eating into margins faster than anyone had calculated.
Here’s what the post-mortem uncovered: over 80% of bag returns traced back to handle stitch failure under dynamic load. Not fabric tears. Not zipper breaks. The handles ripped clean off — often mid-lift on a staircase or loading dock. The fix cost $0.18 per unit. Double-bar tack reinforcement at stress points. That single change eliminated the majority of field failures before anyone even touched the material question. The bigger lesson landed harder: the cheapest bag was nowhere near the cheapest bag to own.
Every failed bag is a liability domino—field rupture triggers crew downtime, damage claims, and safety incidents that compound across a quarter.
The logistics firm in this case was bleeding $12,600 annually on replacement bags alone before the switch. That number, however, understated the full bleed. When a bag seam gives way on a staircase or loading ramp, the immediate consequence is crew downtime. Two workers stop moving, spend 15 minutes repacking a 50 kg load into a fresh bag, and the job timeline stretches. Over a peak season with 200 crew-days, those 15-minute breaks erode 50 hours of billable labor. That’s time clients don’t forgive.
These aren’t theoretical risks. The firm’s incident log showed three lower-back strains in a single month directly linked to bag handle blowouts. One led to a lost-time claim that increased their experience modification factor by 0.15, inflating insurance costs across the fleet. When you factor that into total cost of ownership, a $0.18 reinforcement cost per bag vanishes into decimal dust.
The root cause wasn’t just cheap material. It was a mismatch between the spec sheet and the real-world load cycle.
The procurement lesson here is brutal: a spec sheet without dynamic load test data, without batch-level QC evidence, and without handle reinforcement geometry is a wish list, not a warranty. When you’re evaluating a moving bag supplier, demand ASTM D5034 grab test data at the seam, not just raw fabric tensile. Ask for the failure mode video, not the pass certificate.
| Categoría de costes ocultos | Symptom | Quantifiable Impact | Root Cause |
|---|---|---|---|
| Handle Stitch Failures | 80% of returns traced to handle seams tearing under dynamic load | $11,200 quarterly damage claims; frequent crew downtime | No bar tack or cross-stitch reinforcement at stress points |
| Premature Material Fatigue | 90gsm PP failing at 35 kg dynamic load, far below required 50 kg | Average bag lifespan limited to 5 moves; high replacement frequency | Standard woven PP with no Oxford fabric upgrade or UV coating |
| Batch Quality Inconsistency | 12% post-delivery defect claims, randomly appearing in fleet | Unplanned replacements erode procurement budget; brand reputation risk | No random tensile testing or QC holds at factory gate |
| Excessive Total Ownership Cost | Low unit price masking repeat failures and hidden labor/waste costs | Annual procurement cost of $12,600 before optimization; 60% failure rate | Spec sheets prioritized static burst metrics over real-world dynamic load |
| Fleet-Wide Recall Exposure | Impossible to isolate defective units without traceability | Risk of recalling 5,000 units for a single production flaw; replacement cost escalation | No custom bag numbering or lot-level labeling |
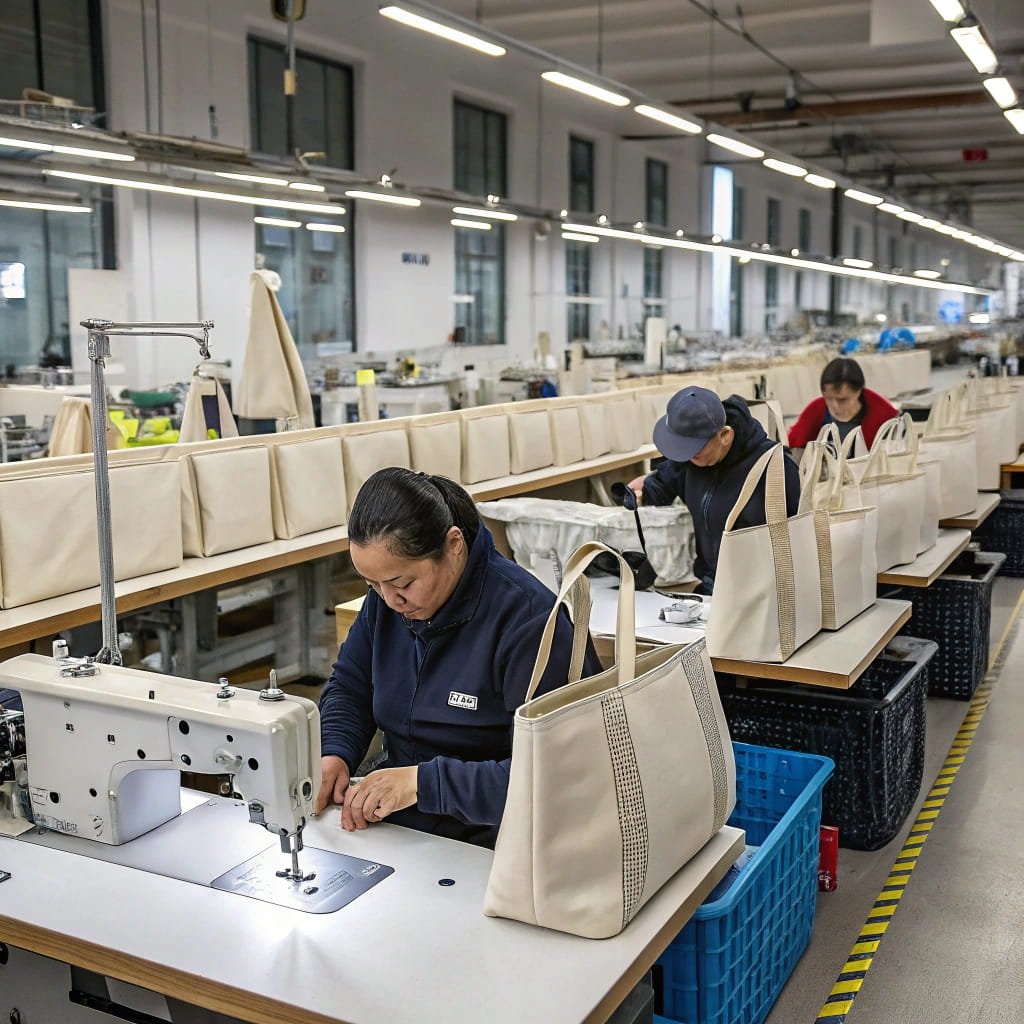
80% of bag returns traced to one failure point: the handle seam under dynamic load.
The existing fleet ran on 90gsm woven polypropylene. Spec sheets looked fine on a desk. In the truck, under a 50 kg dynamic load, the fabric tore at the weave intersection. Switching to 150gsm coated Oxford fabric moved the failure point from 35 kg to beyond 50 kg in repeated drop tests. The PU coating added abrasion resistance and eliminated moisture wicking that softened standard PP after three wet moves. UV inhibitors in the coating prevented degradation during ramp staging in direct sunlight—a failure mode the previous supplier never addressed.
Average usable lifespan jumped from 5 to 12+ heavy-duty cycles. That single material change cut replacement purchasing frequency by more than half, directly reducing annual procurement cost from $12,600 to $2,904 despite a 15% higher unit price.
Handle stress points were the next target. Post-mortem analysis showed 80% of prior-quarter returns originated at the handle attachment. The original single-needle lockstitch created a perforation line that acted like a tear-off coupon when forces shifted suddenly. The fix: double-bar tack reinforcement at all handle anchor zones, using a 301 lockstitch with 12 stitches per inch on a triple-feed walking-foot machine. This distributed load over a 40 mm zone instead of a single stitch row.
Seam strength increased 40% in static pull tests. Dynamic load testing—simulating a bag dropped while gripped by one handle—showed the reinforced design withstood 50 kg without stitch elongation. Handle-related returns dropped by 80% within the first quarter post-change. The added cost: $0.18 per unit.
Even with better materials and stitching, batch variation kills reliability. The previous supplier shipped based on visual inspection only. The logistics firm established a 10% random batch tensile test protocol at the factory gate, using a calibrated frame that pulled handle-to-body seams to failure. Any batch below 45 kg average triggered a full inspection hold and rejection. This single QC gate reduced post-delivery defect claims from 12% to under 2% in one year.
Batch-specific numbering added traceability. When a lot with inadequate coating adhesion slipped through, the numbering system isolated the affected 200 units in 48 hours. Without it, the recall would have swallowed the full 5,000-unit fleet. The root cause was traced to a humidity excursion during curing, corrected at the factory within three days.
| Engineering Area | Previous Standard | Upgraded Specification | Measurable Outcome |
|---|---|---|---|
| Base Material | 90gsm non-reinforced woven PP, no UV coating | 150gsm coated Oxford fabric with UV protection | Lifespan extended from 5 to 12+ heavy-duty moves; dynamic load tolerance raised from 35 kg to 50 kg |
| Costura de las asas | Single-stitch or non-reinforced seam at stress points | Double-bar tack reinforcement with cross-stitch pattern | Seam strength increased by 40%; 80% reduction in handle-related returns |
| Batch Quality Control | No systematic tensile testing before shipment | 10% random batch tensile testing + QC hold gate | Post-delivery defect claims fell from 12% to under 2% in Year 1 |
| Unit Traceability | No individual bag identification | Custom bag numbering for production lot traceability | Identified faulty coating lot immediately; contained recall to 200 units instead of 5,000 |
Rollout success depends on crews using bags within design limits.
The pilot confirmed that switching to 150gsm coated Oxford with double-bar tack reinforcement extended usable cycles from 5 to 12+. That gain evaporates fast if load limits get ignored. Previous 140gsm PP bags failed at 35 kg under dynamic load; the new bags hold 50 kg. Pushing past that threshold still risks handle stitch rupture—the same failure that caused 80% of prior returns.
Traceability gets ignored until a quality crisis hits. This firm printed a unique batch code and sequential number on each bag. When field supervisors noticed coating delamination on a handful of units, the codes instantly isolated a single production lot. The alternative—a fleet-wide recall across 5,000 bags—was avoided by replacing only 200. Handle reinforcement added $0.18 per unit; the numbering added negligible cost while saving an estimated $11,200 in damage claim exposure. Procurement teams that skip custom labeling assume a risk they can’t quantify.

The math hits different when your bags survive 12 moves instead of 5.
Six months after switching to the reinforced bag spec, field failure rates dropped 60%. The average usable life of a bag moved from 5 heavy-duty cycles to over 12. That wasn’t just a durability stat—it redefined what the ops team considered a “consumable.” Bags that used to be thrown away after a handful of jobs were now lasting an entire peak season. The crew stopped hoarding “good” bags and stopped treating every move like a gamble.
The unit price went up 15%—about $0.18 per bag for the handle bar tack alone—but annual procurement cost fell from $12,600 to $2,904. That’s a 40% total cost of ownership decline. The quarterly damage claims budget lost $11,200 in waste and that money stayed on the P&L. Nobody in procurement got pushback on the per-unit increase because the aggregate numbers made the argument for them.
Reputation impact hit two places hard. Insurance adjusters noticed fewer damage claims tied to bag blowouts and started asking what changed. Corporate clients who used to document every torn bag in quality audits stopped seeing moving bag failures show up in their reports. When you’re bidding on contracts with healthcare or high-end residential movers, “zero bag-failure incidents in 12 months” becomes a differentiator that stacks directly against competitors still running on thin-woven PP.
A 60% drop in field failures didn’t come from spending more. It came from spending differently: $0.18 per unit on handle reinforcement eliminated over 80% of returns, and a 10% batch-level tensile hold cut defect claims to under 2%. Annual procurement cost fell 40% while the average bag lifespan more than doubled. The math holds up.
Review current specs for 150gsm coated Oxford fabric, double-bar tack stitching, and batch-level QC holds—the three levers that turned a liability into a procurement win.
La carga estática mide un peso constante suspendido; la carga dinámica simula las sacudidas, oscilaciones y caídas repentinas que se producen en la vida real y que provocan la rotura de las costuras de las asas. El estudio de caso reveló que el 80% presentaba fallos detectados en condiciones reales de uso. Solicita siempre un vídeo de las pruebas dinámicas, no te conformes solo con la capacidad de carga estática.
El precio unitario puede aumentar entre un 15 y un 30%, pero el coste total de propiedad se reduce si se tienen en cuenta los tiempos de inactividad debidos a averías y las reclamaciones. La empresa de logística del caso práctico compensó el... Realiza primero una prueba piloto controlada para validar el retorno de la inversión por bolsa en tu propia operación.
It won’t weaken the bag if heat and pressure are calibrated precisely to the fabric’s tolerance. Poorly controlled printing overheats the base material, degrading tensile strength at stress points like handles. Validate with a seam-strength test on printed samples before bulk production.
Los diseños en stock pueden empezar a partir de 300-500 unidades, mientras que las bolsas reforzadas a medida suelen requerir más de 1.000 unidades para que la preparación del material resulte rentable. La cantidad mínima de pedido (MOQ) varía en función de la complejidad del refuerzo de las asas y de los requisitos de impresión. No se fije la MOQ exacta hasta que se hayan concretado las especificaciones del refuerzo y el material gráfico.
En una flota logística con una media de ciclos diarios, las bolsas debidamente reforzadas aguantan más de 12 traslados, lo que equivale aproximadamente a entre 3 y 6 meses de uso intensivo continuo. El estudio de caso amplió la vida útil media de 5 traslados a más de ese número. Realiza un seguimiento del uso por lotes para planificar los pedidos de reposición antes de que aumenten las tasas de averías.
SOLICITAR PRESUPUESTO
Product, size and quantity is enough to start. We reply with a price and a sample plan fast.
Saved locally for this preview.
